
Atmospheric Corrosion Resistance of TH500NQ-II Welded Joints: Mechanisms and Evaluation Methods
Introduction: Importance of Corrosion Resistance in Weathering Steel Welds
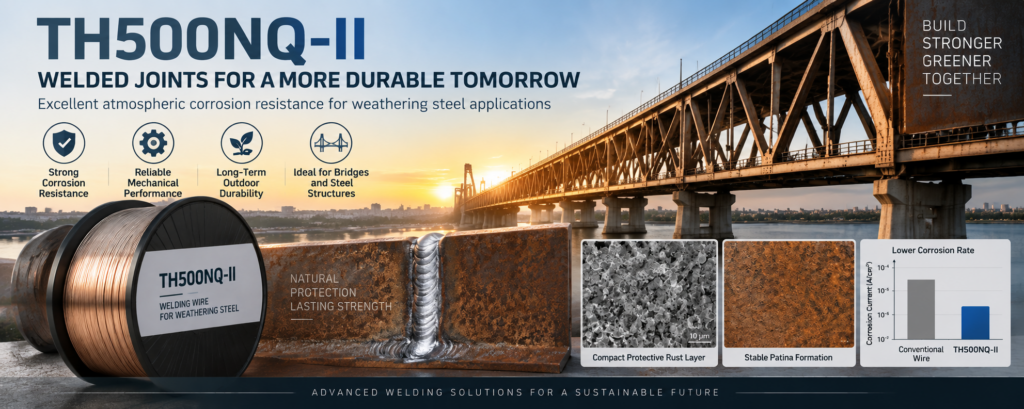
Weathering steel is widely used in outdoor structures because it can develop a stable protective rust layer under atmospheric exposure. Unlike conventional carbon steel, which requires continuous coating protection, weathering steel relies on controlled corrosion processes to form a dense patina layer that reduces further degradation.TH500NQ-II
However, the corrosion resistance of a weathering steel structure is not determined only by the base metal. Welded joints represent critical areas where differences in chemical composition, microstructure, and thermal history may influence long-term atmospheric corrosion behavior.
TH500NQ-II welding wire is specifically designed for welding weathering steel structures. Its alloy composition and deposited weld metal characteristics help maintain compatibility with weather-resistant steel systems by providing balanced mechanical properties and enhanced atmospheric corrosion resistance.
Understanding the corrosion mechanism of TH500NQ-II welded joints is essential for applications such as bridges, railway structures, heavy steel frameworks, and other outdoor engineering components exposed to complex environments.
1. Atmospheric Corrosion Behavior of TH500NQ-II Welded Joints
1.1 Initial Corrosion Process After Welding
After welding, the surface of TH500NQ-II weld metal begins to interact with atmospheric factors including:
Oxygen
Water vapor
Rainwater
Industrial pollutants
Temperature fluctuations
During the initial corrosion stage, unstable iron oxides and hydroxides are generated on the weld surface. These corrosion products are relatively porous and cannot effectively prevent further oxygen and moisture penetration.
With continuous environmental exposure, alloying elements within the weld metal gradually participate in corrosion product transformation, promoting the formation of a more compact protective patina.
The evolution process generally includes:
Formation of active corrosion products
Transformation into stable iron oxyhydroxide phases
Enrichment of alloying elements near the surface
Development of a protective rust layer
A stable patina significantly decreases the electrochemical activity of the weld surface and improves long-term corrosion resistance.
2. Metallurgical Factors Affecting TH500NQ-II Corrosion Resistance
The atmospheric corrosion performance of TH500NQ-II welded joints is closely related to its chemical composition and microstructural characteristics.
2.1 Role of Copper in Protective Rust Formation
Copper is one of the key alloying elements influencing weathering steel corrosion behavior.
During atmospheric exposure, copper gradually enriches within the rust layer and contributes to:
Reduced rust layer permeability
Improved adhesion between corrosion products and steel surface
Suppression of continuous corrosion reactions
Copper-containing corrosion products help create a denser barrier, limiting the transport of oxygen and water toward the underlying metal.
2.2 Influence of Chromium on Rust Stability
Chromium improves the stability of corrosion products by promoting the formation of protective oxide structures.
In TH500NQ-II weld metal, chromium contributes to:
Enhanced oxidation resistance
Increased compactness of the rust layer
Improved corrosion resistance under atmospheric conditions
Chromium-containing compounds reduce the dissolution rate of corrosion products and improve the durability of the protective patina.
2.3 Contribution of Nickel to Atmospheric Durability
Nickel plays an important role in improving corrosion resistance, especially in environments with higher humidity or aggressive atmospheric conditions.
The addition of nickel can enhance:
Rust layer stability
Resistance to cyclic wetting and drying
Structural integrity of corrosion products
This helps TH500NQ-II welded joints maintain stable performance during long-term outdoor service.
3. Microstructure and Corrosion Performance Relationship
The corrosion resistance of welded joints is strongly influenced by weld metal microstructure.
During welding, rapid heating and cooling produce complex metallurgical transformations, including:
Grain refinement
Phase transformation
Redistribution of alloying elements
A well-controlled weld microstructure can improve:
Uniform corrosion behavior
Mechanical stability
Resistance to localized corrosion
Fine and homogeneous microstructures generally provide fewer preferential corrosion paths compared with coarse or heterogeneous structures.
For TH500NQ-II welded joints, optimized alloy design and welding procedures are essential to achieve a balanced relationship between strength, toughness, and atmospheric corrosion resistance.
4. Formation Mechanism of Protective Patina on TH500NQ-II Welds
The protective patina formation process can be divided into several stages.
Stage 1: Active Rust Formation
Immediately after exposure, iron reacts with oxygen and moisture:
Iron → Iron oxides → Iron hydroxides
The initial rust layer is loose and provides limited protection.
Stage 2: Rust Layer Transformation
With increasing exposure time, unstable corrosion products gradually transform into more stable phases, including:
α-FeOOH (goethite)
γ-FeOOH (lepidocrocite)
Fe₃O₄ (magnetite)
Among these phases, compact α-FeOOH contributes significantly to protective behavior.
Stage 3: Protective Layer Stabilization
Alloying elements such as Cu, Cr, and Ni become enriched within the rust layer.
This results in:
Lower ion migration
Reduced oxygen diffusion
Improved rust adhesion
Slower corrosion rate
The final patina acts as a natural protective coating for TH500NQ-II welded joints.
5. Evaluation Methods for TH500NQ-II Atmospheric Corrosion Resistance
Reliable evaluation methods are required to understand long-term corrosion performance.
5.1 Salt Spray Testing
Salt spray testing is commonly used to accelerate corrosion processes.
Key evaluation parameters include:
Corrosion appearance
Rust layer development
Mass loss
Surface morphology changes
Although accelerated tests cannot completely reproduce natural environments, they provide useful comparative information.
5.2 Electrochemical Measurements
Electrochemical techniques provide detailed information about corrosion behavior.
Common methods include:
Electrochemical Impedance Spectroscopy (EIS)
Used to evaluate:
Rust layer resistance
Charge transfer behavior
Protective ability of corrosion products
Polarization Testing
Used to determine:
Corrosion current density
Corrosion potential
Corrosion rate
Lower corrosion current density generally indicates better corrosion resistance.
5.3 Surface and Microstructure Characterization
Advanced characterization techniques can reveal the relationship between corrosion products and metallurgical structure.
Typical methods include:
Scanning Electron Microscopy (SEM)
Used to observe:
Rust morphology
Surface compactness
Crack formation
X-ray Diffraction (XRD)
Used to identify:
Corrosion product phases
Stable oxide formation
Energy Dispersive Spectroscopy (EDS)
Used to analyze:
Distribution of alloying elements
Element enrichment within rust layers
6. Factors Affecting TH500NQ-II Weld Corrosion Performance
Although TH500NQ-II provides excellent corrosion-resistant characteristics, actual performance depends on several engineering factors.
6.1 TH500NQ-II Welding Parameters
Important parameters include:
Welding heat input
Shielding gas composition
Welding speed
Interpass temperature
Improper parameters may alter weld microstructure and influence corrosion behavior.
6.2 TH500NQ-II Environmental Conditions
Atmospheric corrosion resistance is affected by:
Humidity
Chloride contamination
Industrial pollutants
Temperature cycling
Structures located near coastal or highly polluted environments require careful corrosion assessment.
6.3 TH500NQ-II Joint Design and Surface Conditions
Weld geometry and surface quality also influence corrosion behavior.
Important considerations include:
Smooth weld transition
Reduced stress concentration
Proper drainage design
Removal of welding defects
7. Industrial Applications of TH500NQ-II Welded Structures
Due to its combination of strength and corrosion resistance, TH500NQ-II welded joints are suitable for applications requiring long-term outdoor durability, including:
Railway bridges
Highway structures
Architectural steel systems
Heavy industrial equipment
Outdoor steel frameworks
In these applications, maintaining corrosion compatibility between weld metal and base steel is essential for achieving reliable service life.
TH500NQ-II Conclusion
The atmospheric corrosion resistance of TH500NQ-II welded joints is determined by the interaction between alloy composition, weld microstructure, and environmental exposure conditions.
Through controlled alloying design, elements such as copper, chromium, and nickel contribute to the formation of a stable protective patina, reducing corrosion progression and improving long-term durability.
Evaluation methods including electrochemical testing, accelerated corrosion experiments, and surface characterization provide valuable insights into corrosion mechanisms and performance optimization.
For weathering steel structures requiring reliable outdoor service, understanding the corrosion behavior of TH500NQ-II welded joints is essential for improving welding quality, structural durability, and lifecycle performance.