
How E307-15 Electrodes Improve Welding Reliability for High Manganese Steel
Introduction: The Challenges of Welding High Manganese Steel
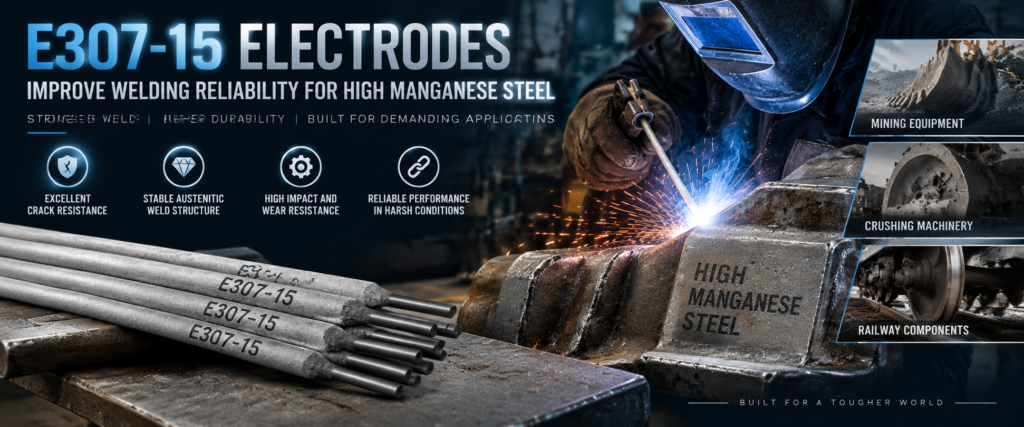
High manganese steel is widely used in demanding industrial environments where components require excellent impact resistance, wear resistance, and long service life. Applications such as mining equipment, crushing machinery, railway components, and heavy-duty structures often rely on the unique properties of manganese steel.E307-15
However, welding high manganese steel presents significant technical challenges.
Unlike conventional steels, high manganese steel has a fully austenitic structure with high work-hardening capability. During welding, the heat-affected zone experiences rapid temperature changes, which may lead to:
Carbide precipitation
Reduced toughness
Thermal cracking
Loss of mechanical properties
Weld joint failure under impact conditions
Therefore, selecting a suitable welding electrode is essential to maintain joint reliability.
E307-15 electrodes are specifically designed to provide a stable austenitic weld deposit with excellent crack resistance and compatibility for difficult-to-weld materials, making them an effective solution for high manganese steel welding applications.
Why High Manganese Steel Is Difficult to Weld
1. Sensitivity to Heat Input
High manganese steel contains a high amount of manganese and carbon, creating a strong austenitic structure with excellent toughness.
However, during welding, excessive heat input can change the microstructure near the weld area.
The main risks include:
Formation of brittle carbide phases
Reduced ductility
Increased crack sensitivity
Lower impact performance
Controlling welding heat is therefore critical when repairing or joining manganese steel components.
A suitable electrode must minimize metallurgical damage while producing a strong and reliable weld.
2. Thermal Cracking Risk
One of the biggest concerns in high manganese steel welding is hot cracking.
During cooling, the weld metal and base metal contract at different rates. This generates internal stress, which may create cracks if the weld structure lacks sufficient ductility.
E307-15 electrodes help reduce this risk by producing a tough austenitic weld metal capable of absorbing welding stress.
The combination of alloy design and controlled weld structure improves resistance against cracking during service conditions.
Metallurgical Advantages of E307-15 Electrodes
Austenitic Weld Structure for Improved Toughness
The performance of E307-15 electrodes comes from their carefully designed alloy system.
The deposited weld metal typically forms an austenitic structure containing chromium, nickel, and manganese alloy elements.
This structure provides:
High ductility
Excellent impact resistance
Good thermal stress tolerance
Improved crack resistance
For high manganese steel applications, maintaining weld toughness is more important than simply increasing hardness.
A ductile weld deposit can better withstand repeated impact and vibration during operation.
Balanced Alloy Design for Reliable Performance
The alloy composition of E307-15 plays an important role in welding reliability.
Chromium: Improving Structural Stability
Chromium contributes to:
Weld corrosion resistance
High-temperature stability
Improved metallurgical performance
It helps maintain the integrity of the weld structure under demanding conditions.
Nickel: Stabilizing Austenitic Microstructure
Nickel is essential for maintaining an austenitic phase.
Its benefits include:
Increased weld ductility
Improved toughness
Better resistance to thermal stress
This makes the weld deposit more suitable for high-impact applications.
Manganese: Enhancing Crack Resistance
Manganese improves:
Austenite stability
Weld metal toughness
Resistance to welding defects
The controlled addition of manganese helps create a balanced weld structure that can handle complex stress conditions.
How E307-15 Improves Welding Reliability
1. Reducing Weld Cracking Problems
Cracking is one of the primary reasons for premature failure in welded manganese steel components.
E307-15 electrodes provide a crack-resistant weld deposit by combining:
Austenitic structure
High ductility
Stable alloy composition
Good stress absorption capability
This allows welded joints to maintain reliability even under repeated impact loading.
2. Maintaining Mechanical Performance After Welding
A successful manganese steel weld must preserve the original advantages of the material.
E307-15 helps maintain:
Impact resistance
Structural toughness
Fatigue performance
Long-term durability
This is especially important for components exposed to continuous mechanical shock.
3. Providing a Reliable Buffer Layer
In many repair applications, E307-15 electrodes can be used as a transition layer before applying wear-resistant materials.
The buffer layer helps:
Improve bonding between base metal and overlay materials
Reduce cracking risks
Absorb stress caused by different material properties
This makes E307-15 a valuable choice for complex repair and rebuilding operations.
Recommended Applications of E307-15 Electrodes
Due to their metallurgical characteristics, E307-15 electrodes are commonly suitable for:
High Manganese Steel Repair
Examples include:
Crusher components
Excavation equipment
Heavy-duty wear parts
Railway components
Dissimilar Metal Welding
E307-15 is also suitable for joining different steel types where conventional electrodes may create compatibility issues.
Typical combinations include:
Austenitic stainless steel and carbon steel
Manganese steel and low-alloy steel
Difficult-to-weld steel combinations
Wear-Resistant Component Manufacturing
For components exposed to impact and vibration, E307-15 provides a tough welding foundation that improves service reliability.
Welding Considerations for E307-15 on High Manganese Steel
Although E307-15 provides excellent weld reliability, proper welding procedures remain essential.
Recommended practices include:
E307-15 Control Heat Input
Excessive heat can negatively affect manganese steel properties.
Operators should maintain:
Appropriate welding current
Controlled interpass temperature
Short welding passes when necessary
E307-15 Proper Surface Preparation
Before welding:
Remove oil and contamination
Clean oxide layers
Inspect for existing cracks
A clean welding surface improves fusion quality and reduces defects.
E307-15 Minimize Welding Stress
Techniques such as controlled bead placement and balanced welding sequences can reduce residual stress and improve joint performance.
E307-15 Conclusion: A Reliable Electrode Solution for High Manganese Steel Welding
Welding high manganese steel requires more than high strength filler material. The key challenge is achieving a balance between toughness, crack resistance, and metallurgical stability.
E307-15 electrodes improve welding reliability through:
Austenitic weld structure
Excellent ductility
Reduced crack sensitivity
Stable alloy performance
Strong compatibility with difficult-to-weld steels
For industrial applications requiring durable and reliable manganese steel welding, E307-15 provides an effective solution for improving weld quality and extending component service life.