
The Role of Ferrite Content in E312-16 Weld Metal Crack Resistance
Introduction
E312-16 stainless steel electrodes are widely recognized for their excellent resistance to weld cracking, especially in applications involving difficult-to-weld materials, high-strength steels, and dissimilar metal joints. One of the key factors behind this performance is the controlled ferrite content within the deposited weld metal.
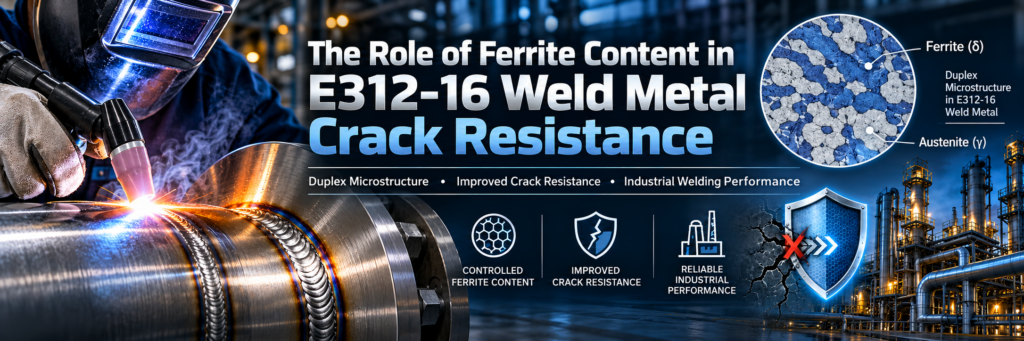
Unlike fully austenitic weld structures, E312-16 develops a ferritic-austenitic duplex microstructure. This balanced structure provides a combination of strength, toughness, and resistance to solidification cracking, making E312-16 suitable for challenging welding conditions.
Understanding how ferrite content influences crack resistance is essential for selecting and applying E312-16 electrodes effectively.
What Is Ferrite Content in E312-16 Weld Metal?
Ferrite content refers to the amount of ferritic phase present in the weld deposit after solidification. In E312-16 weld metal, ferrite exists together with austenite, creating a duplex structure rather than a single-phase microstructure.
During welding, molten metal undergoes rapid cooling and solidification. The final weld structure is influenced by:
Chemical composition of the weld deposit
Chromium and nickel balance
Cooling rate
Dilution from the base metal
Welding heat input
The ferrite phase plays an important role in controlling weld solidification behavior and reducing the risk of hot cracking.
Why Ferrite Improves E312-16 Crack Resistance
1. Reducing Solidification Cracking Risk
Hot cracking is one of the most common problems in stainless steel welding. It usually occurs during the final stage of weld solidification when low-melting elements and impurities concentrate between growing grains.
Ferrite helps reduce this risk by:
Improving the solubility of certain impurity elements
Reducing continuous liquid films along grain boundaries
Promoting a more favorable solidification path
The presence of ferrite in stainless weld metals is commonly associated with improved resistance to solidification cracking because ferrite can interrupt crack propagation paths.
For E312-16 electrodes, the duplex ferritic-austenitic structure provides enhanced tolerance against cracking compared with many fully austenitic weld deposits.
2. Improving Weld Metal Microstructure Stability
The duplex structure of E312-16 contains both:
Austenite phase: Provides ductility and toughness
Ferrite phase: Provides strength and crack resistance
Ferrite acts as a reinforcing phase within the weld metal, improving structural stability under welding stresses.
During cooling, welding generates significant thermal contraction forces. A suitable ferrite level helps the weld metal accommodate these stresses and reduces the possibility of crack formation.
3. Enhancing Performance in High-Restraint Welding
Some welding applications involve severe restraint conditions, including:
Dissimilar metal joints
High-carbon steels
Tool steels
Cast steel repair
Hardenable alloys
These materials often generate higher residual stresses during cooling.
E312-16 is commonly selected for such applications because its ferritic-austenitic weld structure provides greater resistance to weld fissuring and cracking under high restraint conditions.
The Relationship Between Ferrite Level and Weld Performance
Although ferrite improves crack resistance, the amount of ferrite must be carefully controlled.
Too Little Ferrite
A weld deposit with insufficient ferrite may experience:
Increased sensitivity to hot cracking
Higher susceptibility to solidification defects
Reduced tolerance to welding stress
Fully austenitic structures generally have a greater risk of cracking because impurities can concentrate at grain boundaries during solidification.
Excessive Ferrite Content
While higher ferrite content improves crack resistance, excessive ferrite may negatively affect:
Ductility
Impact toughness
Corrosion performance in certain environments
High ferrite levels can also increase the risk of embrittlement during prolonged exposure to specific temperature ranges. Therefore, controlling ferrite balance is essential for achieving reliable weld performance.
How E312-16 Achieves a Duplex Weld Structure
The duplex microstructure of E312-16 is mainly achieved through careful alloy design.
Important alloying elements include:
Chromium (Cr)
Chromium promotes ferrite formation and contributes to:
Corrosion resistance
Oxidation resistance
High-temperature stability
Nickel (Ni)
Nickel stabilizes austenite and improves:
Toughness
Ductility
Weld metal flexibility
Balanced Cr/Ni Equivalent Ratio
The relationship between ferrite-forming and austenite-forming elements determines the final weld structure.
A suitable balance allows E312-16 to solidify with a ferrite-containing structure that improves crack resistance while maintaining mechanical performance.
Applications Benefiting From Ferrite-Controlled E312-16 Weld Metal
Because of its crack-resistant characteristics, E312-16 is frequently used in applications such as:
Dissimilar Metal Welding
Examples include joining:
Stainless steel to carbon steel
Stainless steel to low-alloy steel
Different alloy systems requiring a reliable transition layer
Repair Welding
E312-16 is suitable for repairing:
High-strength components
Tool steels
Cast steels
Components exposed to mechanical stress
Buffer Layers Before Hardfacing
The strong and crack-resistant weld deposit can provide a stable intermediate layer before applying wear-resistant materials.
Welding Considerations for Optimizing Ferrite Performance
To maximize the benefits of ferrite content in E312-16 welding, proper welding practices are important:
E312-16 Control Heat Input
Excessive heat input can alter weld cooling behavior and affect microstructure balance.
E312-16 Maintain Proper Interpass Temperature
Controlling interpass temperature helps prevent undesirable phase changes.
E312-16 Minimize Base Metal Dilution
High dilution may change the chemical balance of the weld deposit and influence ferrite formation.
E312-16 Use Appropriate Welding Parameters
Correct current, voltage, and travel speed help achieve stable weld quality and consistent microstructure.
E312-16 Conclusion
Ferrite content is a critical factor determining the crack resistance of E312-16 weld metal. The controlled ferritic-austenitic duplex structure provides improved resistance to solidification cracking, better stress tolerance, and reliable performance in difficult welding applications.
By balancing ferrite and austenite phases, E312-16 electrodes achieve a combination of strength, toughness, and weld reliability that makes them valuable for dissimilar metal welding, repair welding, and high-stress industrial applications.
Understanding the role of ferrite content allows engineers and welders to optimize welding procedures and achieve more durable, crack-resistant weld joints.